Archives: Published Articles

Susan Schniepp, Regulatory Compliance Associates Inc., discusses digital twins and AI in pharma, focusing on data integrity, human-in-the-loop roles, and evolving machine learning risks in this publication from PharmTech.


Digital Twins

Link to the Video and Article on Pharmaceutical Technology


In part 1 of a 2-part interview (Link to Part 2), and as a part of PDA Week 2026, Susan Schniepp, Regulatory Compliance Associates Inc., discusses the evolving role of technology in the manufacturing landscape. A central focus of her discussion is the implementation of digital twins, which she describes as systems that mimic live operators. Schniepp explains that when these digital models diverge from physical operations, it prompts corrective actions or new validations to bring the two back into alignment. A primary benefit of this technology is the ability to identify data integrity hotspots, areas where violations might occur due to how documents are handled.


The shift toward AI represents a significant change from traditional paper or middle electronic systems where humans perform every approval. With machine learning, the system can now perform much of the data collection and verification itself, allowing the machine to take on a larger role. However, this shift raises critical questions regarding where human oversight is most efficient. Schniepp suggests that discrepancies between human opinion and machine data should be treated as deviations requiring a formal investigation. She notes, “The traditional model that we have is to do an investigation on it.”


Looking ahead, Schniepp acknowledges the rapid pace of machine learning and its potential to surpass human capability in data processing. She observes, “At some point the machine ultimately is probably more capable at looking at some of these things as it learns, it’s gonna absorb so much more data and information and learn at a faster pace than the human can, that at some point the human’s gonna be, and this is where I get concerned, the human will be out of the loop.” For now, she advocates for human precedence, suggesting that because the technology is so new, humans should investigate the digital twin during conflicts to determine the root cause of any discrepancy.
In this video article published by PharmTech, Susan Schniepp says poor quality in pharma manufacturing is costly but catching defects early can saves millions.

Link to the Video and Article on Pharmaceutical Technology


In part 1 of a 3-part interview, Susan Schniepp, Regulatory Compliance Associates Inc., sat down with PharmTech, during PDA Week 2026, to discuss the critical importance of quality systems in pharmaceutical manufacturing. Drawing on her experience participating in PDA planning committees and her work interfacing with the FDA on 503B compounding, Schniepp makes a compelling financial case for investing in quality at every stage of production.


At the heart of her argument is a straightforward cost escalation model tied to where in the manufacturing process a defective material is caught. Catching a problem at incoming inspection costs virtually nothing, the material is simply returned. But the price of missing that defect climbs steeply from there. As Schniepp explained, “It costs you $10,000 if it makes it on your shelf. It costs you $20,000 if it makes it to your floor.” The numbers continue to rise to $50,000 if the defect enters the batch, $100,000 if it reaches final product, and a staggering $1,000,000 if a full field recall becomes necessary.


Beyond the financial toll, Schniepp emphasizes that recalls carry serious reputational consequences regardless of their severity. “It’s the reputation of the company that’s at stake whenever there’s any kind of recall,” she notes, pointing out that even a cosmetic issue like a smeared label can damage how customers perceive a brand.


Ultimately, Schniepp’s message is clear: a robust quality system is not merely a regulatory obligation, it is a sound business investment. By catching problems early and consistently, companies can avoid the exponentially higher costs that come with letting defects slip through the cracks.

Preventing Pharmaceutical Product Recalls

In this episode of Ask the Expert, Susan J. Schniepp of Regulatory Compliance Associates (RCA), a Nelson Labs company, and Siegfried Schmitt of Parexel discuss common causes of pharmaceutical product recalls and strategies for prevention. Key drivers include microbial contamination, mislabeling, and physical contaminants such as glass particulates. Despite established quality systems, vulnerabilities involving subcontractors, production pressures, and human error can still lead to product quality failures.


The experts emphasize the importance of proactive quality oversight and effective investigation procedures. Microbial contamination requires a comprehensive contamination control strategy that integrates environmental monitoring, personnel monitoring, and water system data. Mislabeling risks can arise from seemingly minor process weaknesses, such as temporary handwritten labels and inadequate controls during product handling. Quality teams should actively engage with manufacturing operations to identify and address these vulnerabilities.


Preventing recalls requires more than documented procedures. Manufacturers should regularly test recall processes to ensure products can be traced and retrieved across complex global supply chains. By applying risk-based quality management principles, strengthening controls throughout manufacturing, and maintaining an integrated quality system, companies can improve oversight, reduce the risk of product quality failures, and better protect patient safety.

Watch the video: Preventing Pharmaceutical Product Recalls


Preventing Pharmaceutical Product Recalls

Navigating the Orphan Drug Development Pathway

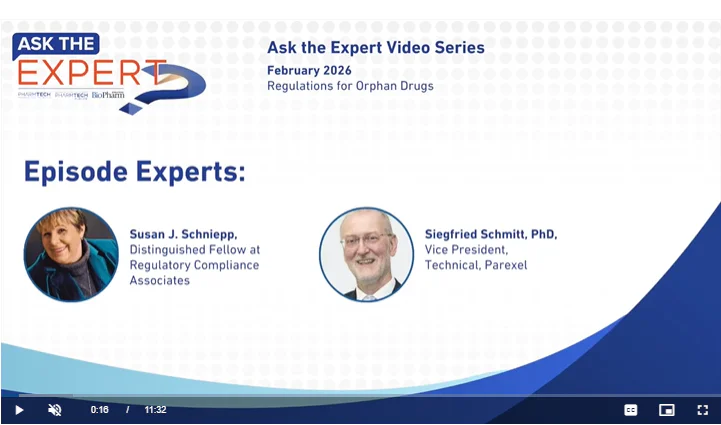
In this episode of Ask the Expert, Susan J. Schniepp of Regulatory Compliance Associates (RCA), a Nelson Labs company, and Siegfried Schmitt of Parexel discuss regulatory considerations for medium-sized pharmaceutical companies pursuing orphan drug development. The experts explore the unique challenges of developing treatments for rare diseases, including regulatory engagement, clinical development, manufacturing, and commercialization.


Orphan drug designation offers incentives intended to support the development of treatments for small patient populations. These may include grants, tax credits, fee waivers, and additional regulatory support. However, orphan drugs must meet the same rigorous quality and compliance standards as traditional pharmaceutical products, requiring companies to establish effective quality systems and maintain regulatory readiness throughout development.


The experts also highlight operational challenges, including small-batch manufacturing, reliance on contract development and manufacturing organizations (CDMOs), global distribution, and patient recruitment for clinical trials. Companies with limited internal regulatory experience should consider seeking external expertise and maintaining close collaboration with regulatory authorities. Early planning and a flexible development strategy can help companies navigate these challenges while supporting the development of treatments for patients with rare diseases.


Watch the video: Navigating the Orphan Drug Development Pathway


Navigating the Orphan Drug Development Pathway


Building a Secure and Resilient Pharmaceutical Supply Chain

In this article, Jane Zhang, Co-Founder and Co-CEO of ETCH Sourcing, and Susan J. Schniepp of Regulatory Compliance Associates (RCA), a Nelson Labs company, discuss strategies for establishing a secure and reliable supply chain early in product development. The experts emphasize that supply chain vulnerabilities often originate during development when purchasing decisions are made without sufficient collaboration across development, quality, and procurement teams.


The article highlights the importance of cross-functional supplier management throughout the product lifecycle. Development teams should work with purchasing and quality to define supplier selection criteria, establish qualification and approval processes, implement quality agreements, and create ongoing supplier performance monitoring procedures. Clear accountability and communication among departments help ensure that supplier decisions address quality, regulatory compliance, reliability, and cost considerations.


The experts also emphasize the value of treating procurement as a strategic partner rather than a transactional function. Development teams define product requirements and performance needs, quality teams determine supplier acceptability, and purchasing teams identify reliable, qualified suppliers. By establishing documented procedures, clear responsibilities, and proactive supplier relationships early, organizations can build a more resilient supply chain and reduce the risk of costly disruptions as products advance toward commercialization.


Read the full article: Building a Secure and Resilient Pharmaceutical Supply Chain


Build a Supply Chain That Supports Quality From Day One

Secure supply chains don’t happen by accident they are designed early through strong purchasing controls, cross functional collaboration, and proactive supplier qualification. Regulatory Compliance Associates® works with pharmaceutical and medical device manufacturers to strengthen supplier oversight, purchasing procedures, and quality agreements that protect product integrity across the lifecycle.


If you’re developing a new product or reevaluating your supplier strategy, RCA can help you design a resilient, compliant supply chain from the start.

Connect with our experts: https://www.rcainc.com/contact-us/

Pharmaceutical Batch Recovery Procedures

In this article, Susan J. Schniepp of Regulatory Compliance Associates (RCA), a Nelson Labs company, discusses best practices for recovering pharmaceutical manufacturing batches following production deviations. Batch recovery involves investigating and correcting identified issues to determine whether a batch can meet established quality, safety, and regulatory requirements. A thorough investigation, including root cause analysis and corrective and preventive actions (CAPAs), is essential to determining whether recovery is appropriate.


The article emphasizes the importance of a robust quality management system to support batch recovery decisions. Effective procedures should include risk assessments, comprehensive documentation, change control, trained personnel, data integrity controls, and collaboration between quality assurance and production teams. Timely investigations and clear communication are particularly important for time-sensitive products that may degrade while awaiting a recovery decision.


Schniepp also highlights that batch recovery is not appropriate in every situation. Decisions should be based on the severity of the deviation and whether the root cause has been conclusively identified and supported by documented evidence. Batches with multiple deviations should not be considered suitable for recovery. Ultimately, proactive quality management, thorough investigations, and continuous improvement can help prevent recurring issues while supporting product integrity and patient safety.


Read the full article: Pharmaceutical Batch Recovery Procedures


Article details

Pharmaceutical Technology®
Vol. 49, No. 9
Page: 26


Citation

When referring to this article, please cite it as Schniepp, S.J. Fundamentals of Batch Recovery Procedures. Pharmaceutical Technology 2025 49 (9).


Partner With Experts Who Strengthen Your Quality & Compliance Framework

Batch recovery decisions demand deep technical expertise, disciplined investigation practices, and a mature quality culture. Regulatory Compliance Associates® helps pharmaceutical manufacturers navigate complex deviations, strengthen root cause analysis, and build the robust quality systems needed to prevent issues before they occur.


If your team needs support with investigations, remediation, or elevating your overall quality and compliance maturity, RCA is here to help.

Learn more or connect with our experts today: https://www.rcainc.com/contact-us/